 Sign up with Google
 Sign in with Zoho
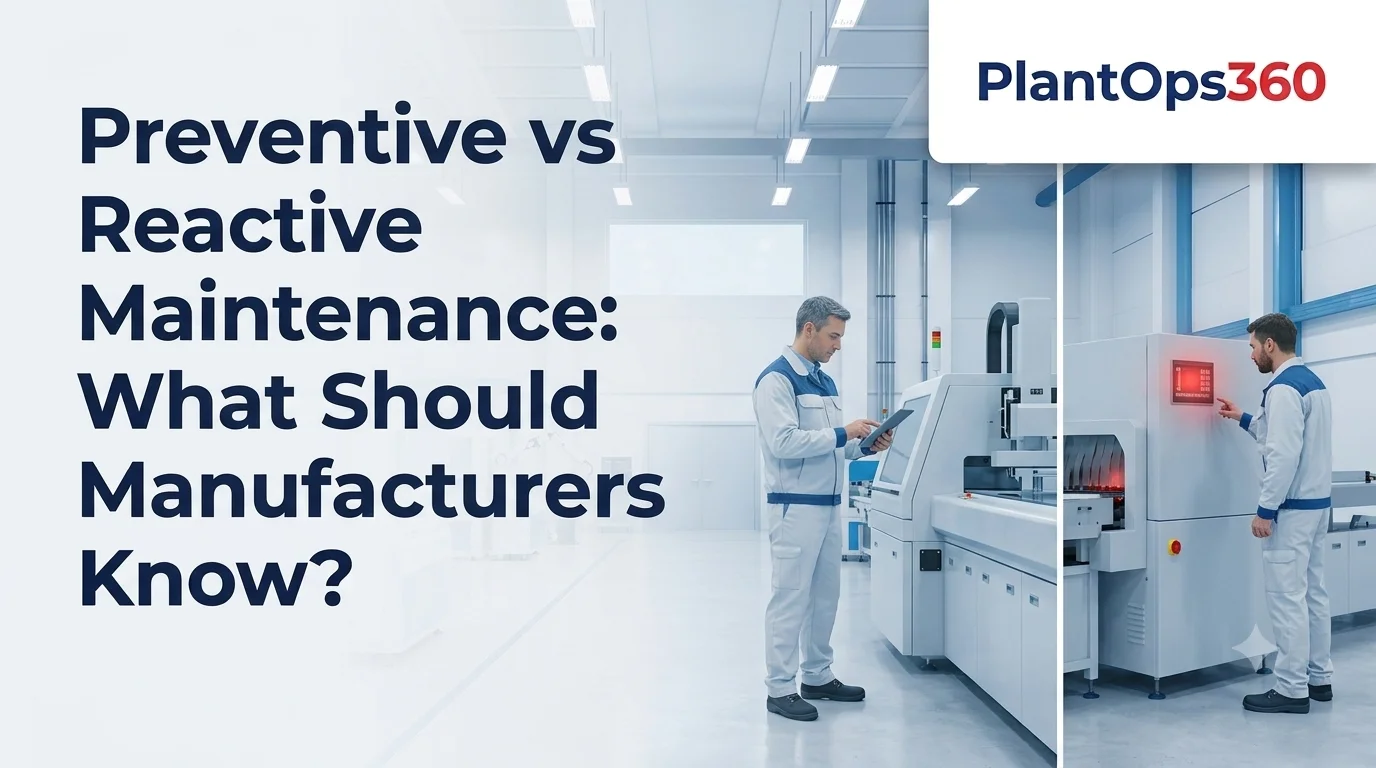
Manufacturers often face one basic maintenance question: should equipment be serviced before it fails, or repaired only after a breakdown? Preventive maintenance plans work before failure happens, while reactive maintenance responds after equipment stops working.
For most plants, the best strategy is not choosing one approach for every asset. The goal is to use planned maintenance where failure creates risk, while keeping reactive maintenance for low-criticality items. PM maintenance software can make that balance easier to manage.
What Is Preventive Maintenance?
Preventive maintenance is planned work performed at regular intervals to reduce the chance of equipment failure. Tasks may be scheduled by calendar time, runtime hours, production cycles, inspections, or other defined triggers.
Typical preventive tasks include:
- Lubrication and cleaning
- Belt and filter replacement
- Safety inspections
- Electrical checks
- Alignment and tightening
- Routine servicing
The main purpose is to prevent problems before they interrupt production.
With PM maintenance software, teams can schedule recurring jobs, assign technicians, record completed work, and maintain a reliable service history without depending on spreadsheets or paper reminders.
What Is Reactive Maintenance?
Reactive maintenance happens after equipment develops a fault or stops working. The maintenance team responds, diagnoses the cause, completes the repair, and returns the asset to service.
This approach can make sense for inexpensive, non-critical equipment where failure has little impact on safety, quality, or production.
Problems arise when reactive work becomes normal for important production assets. Emergency repairs can disrupt labor, spare-parts availability, and production schedules.
Preventive vs Reactive Maintenance: What Is the Main Difference?
The main difference is when maintenance takes place.
Preventive Maintenance Acts Before Failure
Preventive maintenance uses planned schedules and defined tasks. Teams know what work is coming and can prepare technicians, tools, and spare parts in advance.
This creates a more predictable maintenance environment and better visibility into upcoming workloads.
Reactive Maintenance Acts After Failure
Reactive maintenance begins when something has already gone wrong. Teams may have to change priorities quickly, find technicians, source parts, and coordinate with production.
For low-risk assets, this may be acceptable. For critical machines, repeated reactive maintenance can create avoidable disruption.
How Does PM Maintenance Software Support Preventive Work?
As the number of assets grows, manually managing recurring maintenance becomes difficult. PM maintenance software creates a central system for planning and tracking scheduled work.
Instead of relying on individual calendars or memory, teams can define maintenance frequencies for each asset and generate work orders when tasks become due.
A structured system can help teams:
- View upcoming maintenance
- Assign work to technicians
- Use standard checklists
- Record completed tasks
- Review equipment history
- Identify overdue work
- Plan labor and spare parts
This makes preventive maintenance easier to standardize across machines, departments, and locations.
Should Manufacturers Stop Using Reactive Maintenance Completely?
No. A strong maintenance strategy usually combines approaches based on asset criticality.
Use Preventive Maintenance for Critical Assets
Preventive maintenance is generally more suitable when equipment failure could:
- Stop an important production line
- Create a safety concern
- Affect product quality
- Cause expensive secondary damage
- Lead to compliance problems
These assets benefit from regular inspection and planned servicing.
Keep Reactive Maintenance for Low-Criticality Assets
A run-to-failure approach can be reasonable for simple equipment that is inexpensive, easy to replace, and unlikely to affect operations.
The important point is to make the decision intentionally. Reactive maintenance should be a planned strategy, not the result of missed schedules or poor visibility.
How Can Manufacturers Find the Right Maintenance Balance?
Start by classifying assets according to operational importance. Consider the impact of failure on production, safety, quality, repair cost, and replacement time.
A practical process is:
- List important production assets.
- Review breakdown and maintenance records.
- Rank assets by failure impact.
- Define preventive tasks for critical equipment.
- Allow run-to-failure where risk is low.
- Review results and adjust frequencies over time.
PM maintenance software can make this easier because teams have schedules, work history, and completion records in one place.
What Should You Look for in PM Maintenance Software?
Software should make maintenance easier for technicians and managers, not add unnecessary administration.
Look for capabilities such as:
- Time-based maintenance scheduling
- Usage or meter-based triggers
- Automatic work order creation
- Reusable task checklists
- Maintenance calendars
- Asset service history
- Overdue maintenance alerts
- Mobile access
- KPI reporting
Ease of use also matters. A system provides little value if technicians avoid updating it.
Frequently Asked Questions
How often should preventive maintenance be scheduled?
The correct frequency depends on the equipment, operating conditions, manufacturer recommendations, and failure history. Start with documented requirements, then adjust intervals using actual maintenance data.
Is preventive maintenance suitable for every machine?
No. Some low-cost or non-critical assets may be more economical to repair after failure. Criticality, safety impact, downtime risk, and repair cost should guide the decision.
What is the difference between preventive and predictive maintenance?
Preventive maintenance follows a planned schedule or usage interval. Predictive maintenance uses condition data and trends to estimate when equipment may need attention before failure.
Can preventive maintenance reduce spare-parts emergencies?
Yes. Planned maintenance gives teams better visibility into upcoming work, so commonly required parts can be prepared before the job instead of sourced urgently after a breakdown.
Conclusion: Move from Firefighting to Planned Maintenance
Preventive and reactive maintenance both have a place in manufacturing. The key is using each approach where it makes operational and financial sense.
Critical assets usually benefit from planned servicing, while selected low-risk equipment may remain suitable for reactive maintenance. A structured system helps teams manage this balance as the plant grows.
If you want to schedule recurring maintenance, track work completion, and build a more organized maintenance program, explore PlantOps360 PM maintenance software for a more proactive approach to plant maintenance.