 Sign up with Google
 Sign in with Zoho
You ran your numbers through the OEE calculator and got a percentage. But a percentage is hard to act on. A manager hears “68% OEE” and asks what it means in minutes, in parts and in money. This guide shows how to turn the three factors into lost time and lost output, and how to decide what to investigate first.
Why 80%, 90% and 95% Are Not Equal Losses
Availability, performance and quality are multiplied, so each factor hurts OEE, but they do not hurt the same amount of production. A 5% quality drop and a 5% availability drop look similar on screen. On the shop floor they come from different problems and cost different amounts of time.
The fix is to convert each factor into the time it costs you.
Convert Each Factor Into Lost Time
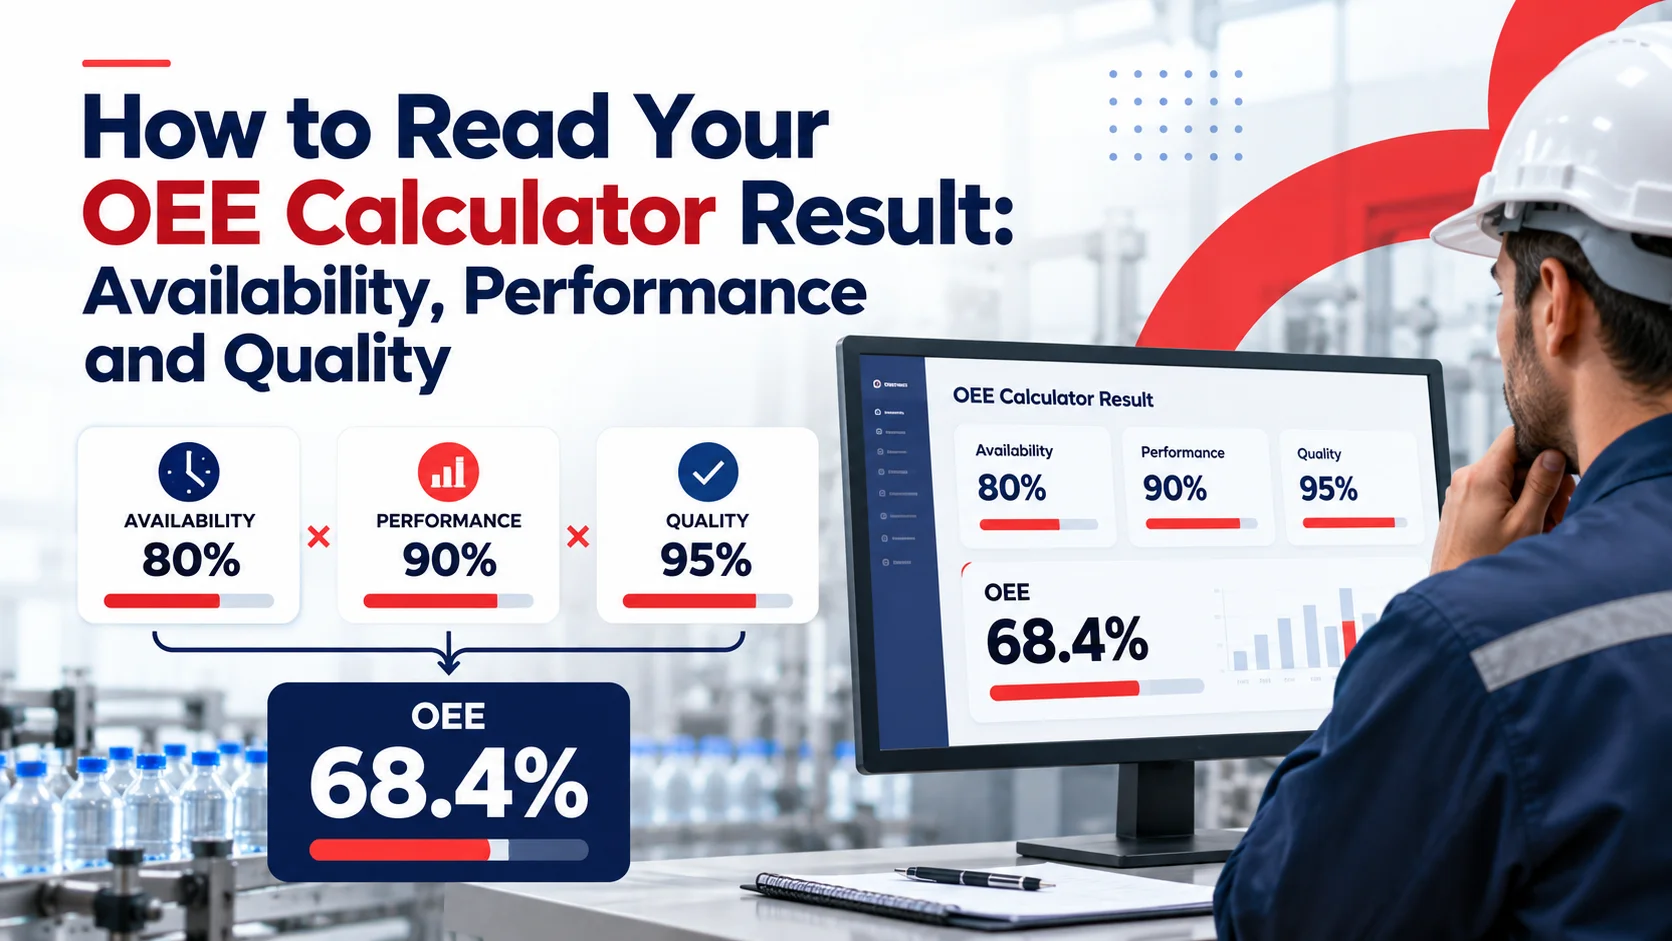
Take a bottle filling line. The ideal rate is 60 bottles a minute. In a 480-minute shift, 60 minutes are planned stops, so planned production time is 420 minutes. The calculator shows:
- Availability 80%
- Performance 90%
- Quality 95%
- OEE 68.4%
Now translate each factor into minutes:
Added together, the line lost about 133 minutes. That leaves 287 minutes of fully productive time, which is 68.4% of 420. The OEE figure is now something you can picture: this line made good bottles at full speed for under five hours of a seven-hour production window.
This view also shows where to look. Availability is the biggest loss here, at more than half of the lost time. Quality, which feels like a small problem at 95%, is the smallest.
Reading Availability: Ask “Which Stops?”
Availability tells you how long the machine stood still. The useful question is which stops.
- Many short stops point to jams, sensor faults or material feed problems.
- A few long stops point to breakdowns, slow repairs or waiting for spares.
- Stops at regular times point to changeovers, cleaning or shift handovers.
In the filling line, 84 minutes could be one gearbox failure or twenty small jams. The fixes are completely different, so record each stop with a time and a reason before you decide.
Reading Performance: Ask “Why Slower?”
A performance loss means the machine ran, but not at full pace. Unlike downtime, nobody writes it down, so it hides well.
Ask the operator what they do differently from the nameplate speed. Typical answers include running slower to avoid jams, reducing speed on a new batch of material or easing off a worn part. Each answer points to a different action: fix the jam cause, review the material specification or replace the worn part.
If performance is well below the other two factors, small stops are the first thing to count. They are rarely logged and often add up to a large share of lost time.
Reading Quality: Ask “When Do Rejects Happen?”
The timing of rejects tells you more than the count. Look at when they occur:
- Right after a restart or changeover: the start-up routine needs work.
- Gradually through a run: a tool, die or nozzle is wearing.
- Randomly across the shift: the cause is likely material or settings.
In the filling line, 907 rejected bottles could come from a fill-level sensor that has drifted, a capper that loosens over time or a bad batch of caps. A short log of when each reject occurred narrows this quickly.
Quick Reference: Symptom to First Check
Common Ways People Misread the Result
- Comparing one shift with another. A shift with a long breakdown will look worse for reasons unrelated to the crew. Compare several shifts before drawing conclusions.
- Averaging machines. A plant average hides the one machine dragging everything down. Read results per machine.
- Celebrating a high quality figure. Quality at 98% sounds good, but if a rejected batch is counted as reworked, it is inflated.
- Chasing the lowest percentage, not the largest time loss. Convert to minutes first, as shown above.
For specific actions once you know where the loss sits, see our guide on how to improve OEE through maintenance.
Frequently Asked Questions
Why does my OEE look low when each factor looks fine?
Because the factors multiply. Three values of 90% each give an OEE of 72.9%, so several small losses together can look large.
Is a 5% improvement in one factor worth the same as in another?
Not in lost time. A 5% availability gain recovers a fifth of the time that a 25% loss would cost, while the same gain in quality recovers the output from the rejected parts. Convert each to minutes to compare.
Should I read OEE for every machine?
Read it for the machines that limit your output first. A gain on a bottleneck machine raises plant output, while a gain on a machine that waits for others does not.
Turn the Reading Into a Decision
Once your result is expressed in minutes and linked to a likely cause, you know what to investigate and why. Record the stops, rejects and speed changes for one week, then act on the largest loss.
If you want help reading OEE across several machines, book a free 30-minute OEE review with PlantOps360 and our team will go through your results with you.