 Sign up with Google
 Sign in with Zoho
A fresh coat of paint can make steel look finished, but its appearance says little about how long the coating will last. If the metal underneath still has grease, loose rust, or moisture on it, problems can develop even when the paint was applied correctly.
Surface preparation is often where these problems begin. A railing might look clean after someone wipes it down, yet still have mill scale around the welds. A steel panel stored outdoors might feel dry while condensation remains along its lower edge.
The work needed before painting depends on the metal, its condition, and the coating being used. Knowing what to remove, what to measure, and when to stop preparation can prevent unnecessary rework.
Know what kind of steel surface you are dealing with
Not every steel surface needs the same treatment.
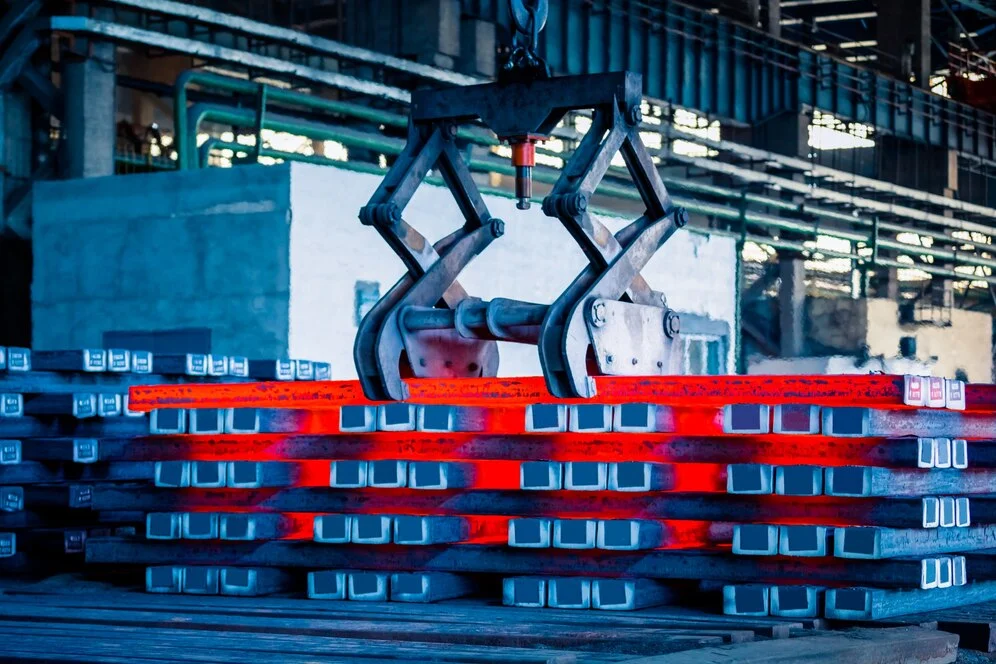
New hot-rolled carbon steel often arrives with mill scale, a dark layer formed during manufacturing. Galvanized steel has a zinc coating that requires different preparation. Previously painted steel presents another set of concerns, particularly when the old coating is peeling or its composition is unknown.
Start by checking the coating manufacturer's technical data sheet. It should identify the required surface cleanliness, acceptable preparation methods, and conditions for applying the product.
The location and intended use of the finished component matter, too. A steel gate exposed to outdoor weather may need a different coating system from a bracket installed inside a dry workshop.
For regional material context, Curtis Steel & Aluminum Co. maintains a St. George page describing metal supply and processing options. The distinction between material types matters because a cleaning method suitable for carbon steel may not be appropriate for stainless or galvanized surfaces.
Before any work begins, identify the base material and confirm which coating system it will receive.
Deal with grease and oil before removing rust
A common preparation mistake is reaching for a grinder or wire brush before checking whether the surface is contaminated with oil.
Steel can carry cutting fluids, handling residue, grease, and other substances that are not immediately obvious. Mechanical cleaning may spread these contaminants rather than remove them.
The Association for Materials Protection and Performance (AMPP) maintains SSPC-SP 1, a standard covering solvent cleaning methods used to remove visible oil, grease, and similar contaminants.
For routine cleaning, begin by removing loose dirt. Check around drilled holes, cut edges, and areas where equipment has contacted the steel.
Use a cleaner compatible with the metal and intended coating. Remove loosened contaminants with clean materials rather than repeatedly wiping the surface with a dirty cloth.
Some cleaning products require rinsing, while others have different removal instructions. Follow the product directions and allow the steel to dry before continuing.
Solvents and chemical cleaners also require appropriate ventilation, protective equipment, and safe handling.
Choose a rust removal method that matches the job
Rust removal is not simply a matter of making steel look shiny.
A wire brush may remove loose oxidation from a small repair area, but it will not necessarily produce the surface condition required for an industrial coating.
Hand tools are useful for certain maintenance tasks. Scrapers and wire brushes can remove loose material where the specification allows this level of preparation.
Power tools can handle more stubborn corrosion and existing coatings. However, grinding can leave smooth areas that may not provide the surface texture required by the primer.
Abrasive blasting removes surface material and can create a controlled texture. It is often specified where a particular level of cleanliness and surface profile is required.
Consider an older steel handrail with patches of rust around its welded joints. The appropriate preparation depends on whether the existing coating is sound, how much corrosion is present, and what the new coating requires.
There is no single cleaning method suitable for every situation. Previously coated steel also needs an assessment for potentially hazardous coating materials before sanding, grinding, or blasting.
Pay attention to the texture left behind
Steel can look clean and still be poorly prepared for painting.
Many protective coatings need a particular surface profile. This refers to the small peaks and valleys left by abrasive preparation.
A surface that is too smooth may not provide sufficient mechanical adhesion for a coating designed to grip a blasted profile. Excessively rough steel creates another problem because the coating may not adequately cover the highest peaks.
The coating manufacturer's instructions should specify the acceptable profile range when one is required.
Inspectors can measure surface profile using instruments such as replica tape or suitable profile gauges.
Take measurements at representative points rather than relying on one convenient location.
A steel plate may have different surface characteristics near its edges than across its center, particularly if separate cleaning methods were used.
Cleanliness and texture should be checked independently. One does not automatically confirm the other.
Watch for moisture even in desert conditions
Steel preparation in St. George or Las Vegas comes with an environmental consideration that is easy to overlook: dry weather does not guarantee dry metal.
Steel exposed to cooler nighttime temperatures can develop condensation when surrounding conditions change. A surface may also remain cooler than the air around it.
This matters because moisture trapped beneath a coating can contribute to adhesion problems and corrosion.
Before applying primer, check the steel surface temperature, air temperature, relative humidity, and dew point.
Do not rely on how the surface feels to the touch. Use suitable measuring equipment and follow the coating manufacturer's environmental limits.
Dust presents another challenge in dry regions.
Nearby grinding, vehicle movement, or construction activity can leave fine particles on recently cleaned steel. Even a thin layer may interfere with coating contact.
After surface preparation, remove accumulated dust using a method permitted by the coating specification.
Avoid leaving freshly blasted carbon steel exposed longer than necessary. Moisture can cause flash rust before the primer is applied.
Finish cutting and welding before the final cleaning
The order of fabrication work can make surface preparation easier or create additional work.
Suppose a steel frame is cleaned and primed before its final brackets are welded into place. Welding may damage the nearby coating, while the new joints introduce spatter and surface deposits that need attention.
For many projects, it makes more sense to complete cutting, drilling, welding, and other fabrication operations before the final preparation stage.
Once fabrication is complete, examine welded joints, corners, drilled openings, and cut edges.
Weld spatter and sharp projections may need removal. Some edges require additional preparation because coatings tend to have difficulty maintaining adequate thickness over sharp corners.
Follow the specified edge preparation requirements rather than removing material unnecessarily.
If further fabrication takes place after coating, affected areas should be repaired using the approved coating procedure.
Give the steel one last inspection before painting
The final inspection should take place after cleaning and before primer application.
Good lighting makes it easier to see remaining rust, dust, loose scale, or areas that were missed during preparation.
Start with welds and corners. These locations can retain debris even when the larger surfaces appear clean.
Next, examine flat areas for contamination and verify the required surface profile where applicable.
AMPP surface preparation standards describe different cleaning methods and cleanliness requirements. The specified standard should guide acceptance rather than a general impression that the steel looks ready.
Before coating begins, confirm the following:
- The required surface cleanliness has been achieved.
- Oil, grease, dust, and loose material have been removed.
- The surface profile meets the coating requirements.
- Welds and edges have received the necessary preparation.
- Temperature and moisture conditions are acceptable.
- No new contamination has settled on the steel.
Some projects also require testing for soluble salts or other contaminants that cannot be identified through visual inspection alone.
If an area does not meet the requirements, correct it before painting. Applying primer over a questionable surface usually makes the underlying problem harder to address.
Keep the prepared surface protected until coating
Steel preparation does not end when the cleaning equipment is switched off.
A properly cleaned surface can become contaminated again through handling, airborne dust, moisture, or nearby workshop activity.
The time between preparation and coating should therefore be managed according to the project specification and coating manufacturer's instructions.
The important distinction is between steel that merely looks clean and steel that meets the required conditions for coating. Surface cleanliness, texture, and environmental conditions all need to be considered before painting begins.

.webp)